 English
 中文简体
 русский
 Español

Gate Location Sets the Whole Tool Up
Gate position decides where plastic enters the cavity, and that single choice influences fill balance, weld line placement, and how much packing pressure the part needs. On a visible interior component, a gate placed in a hidden area keeps the surface clean, but it may push flow length longer and demand more injection pressure. A gate moved closer to the centre fills faster but can leave a mark where the customer will see it.
When reviewing an automotive plastic mould quotation, ask where the gate sits and what trade-off drove that choice. Suppliers who explain the flow analysis behind the gate location are usually the ones who have already thought through the part's cosmetic requirements, not just the tool's ease of machining.
Runner Layout Affects Scrap and Cycle Spread
Cold runners and hot runners have different cost profiles over a tool's life. A cold runner system is simpler to build and easier to troubleshoot, but it produces sprue and runner scrap that has to be reground or discarded. A hot runner keeps melt at temperature all the way to the gate and reduces scrap, though it adds complexity and needs careful thermal zoning.
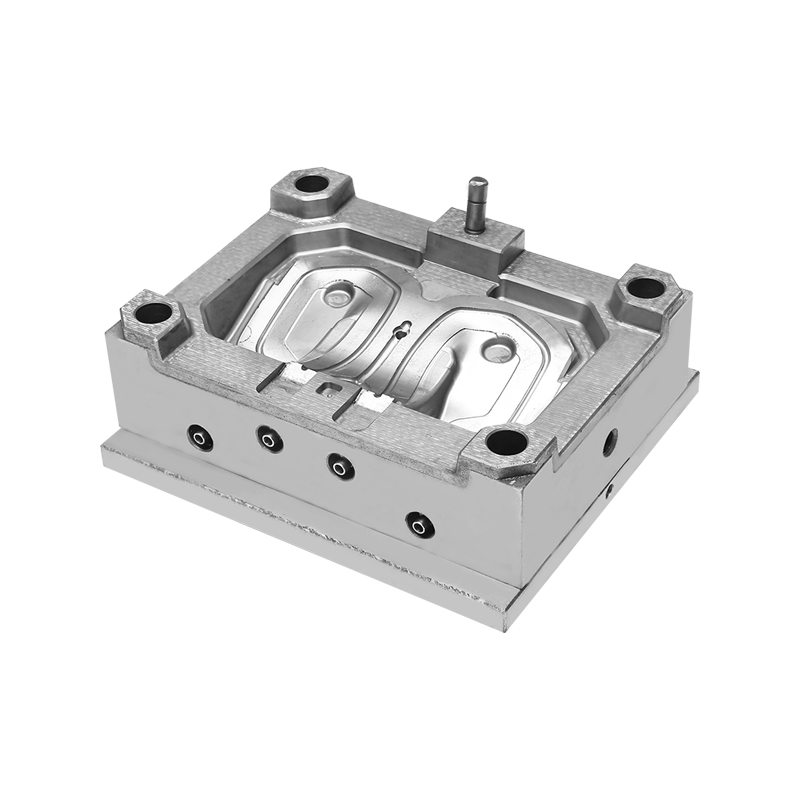
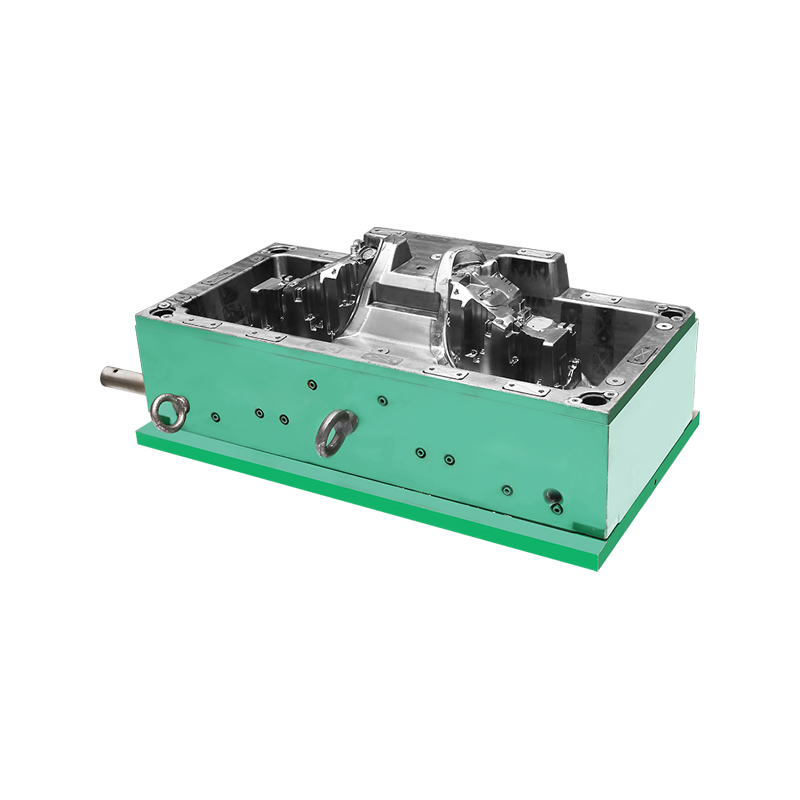
For an automotive plastic mould running a family of small brackets, the runner decision often comes down to volume and material cost. For a large single part, the question shifts to whether a hot runner drop can be placed without creating flow marks. Buyers should confirm the runner type in writing and ask how many drops or gates the design uses.
Cooling Layout Drives Cycle Consistency
Cooling channels are invisible once the tool is assembled, yet they shape cycle time and dimensional stability more than many buyers expect. Channels placed too far from the cavity surface slow heat removal; channels placed unevenly cause parts to warp as they cool. Baffles and bubblers allow cooling in deep cores, but they add machining steps and need clean water flow to stay effective.
A practical question for any automotive plastic mould supplier is how the cooling layout was checked. Conformal cooling or simulation-backed channel routing costs more at the design stage, but it often shortens cycle time on parts with thick sections. Buyers comparing two quotations with different cooling approaches are effectively comparing two different production costs.
Ejection and Part Geometry Need to Agree
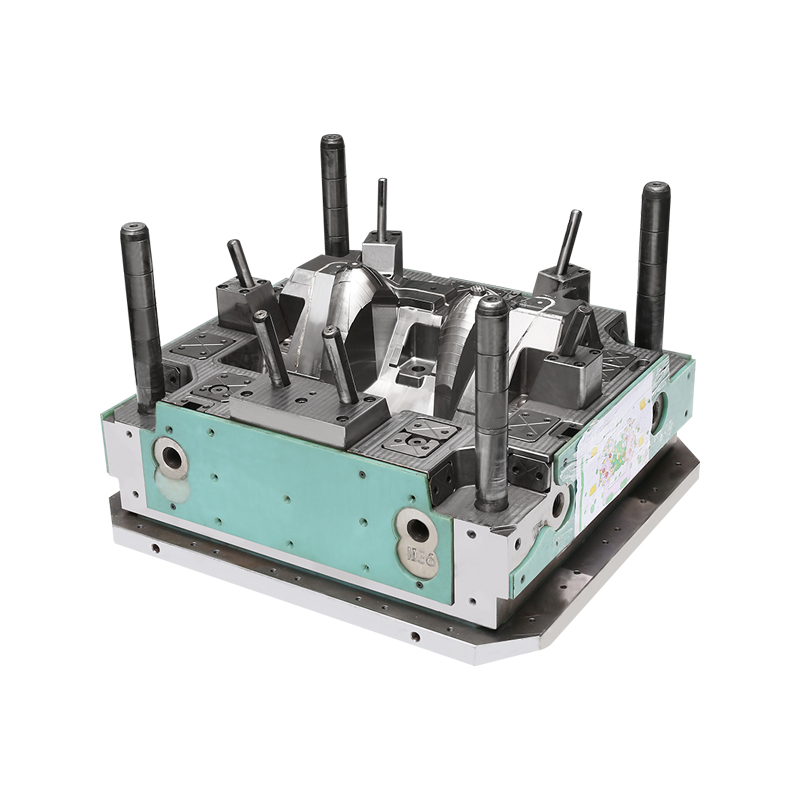
Ejection design follows part geometry. A part with thin walls and deep ribs needs ejector pins placed where they will not mark or distort the surface. Sleeve ejection suits cylindrical features, while stripper plates work well for shallow, wide parts. On an automotive plastic mould producing clips or fasteners, ejector placement can be the difference between a clean release and a part that sticks and tears.
Buyers should ask for the ejection layout and check it against the part drawing. If the supplier cannot explain how the part will release without stress marks, that is worth resolving before the tool is cut rather than after the trial.
Steel and Insert Choices Tie Back to Volume
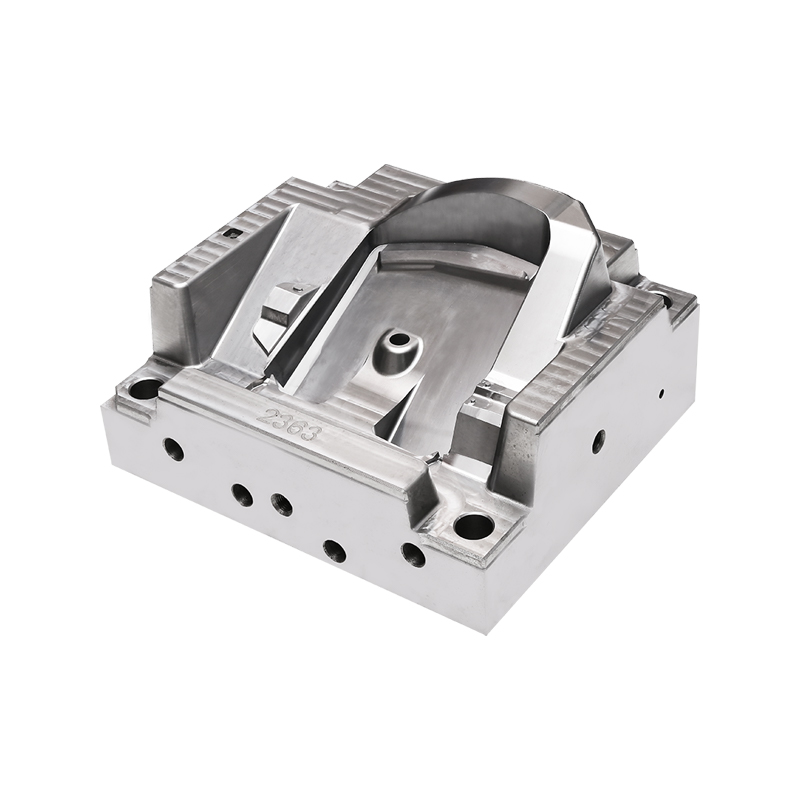
The steel specified for the cavity and core should match the production volume and the resin being run. Abrasive glass-filled resins wear softer steels faster, and high-volume programmes justify harder cavity steels or inserts that can be replaced without scrapping the whole tool. An automotive plastic mould built for a short pilot run may use different steel than one intended for years of production.
Insert design is part of the same decision. Replaceable inserts for high-wear areas keep an automotive plastic mould in service longer without a full rebuild. Buyers should confirm which areas are inserted and what steel grade sits in each.